Non-standard automated equipment
Non-standard automated equipment
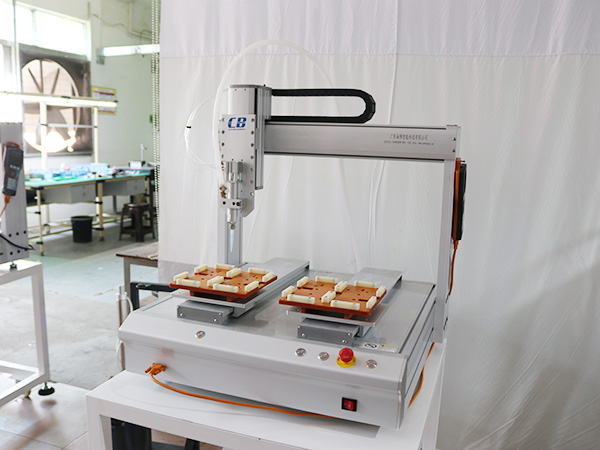
Due to the requirements of the process, some products must use high-viscosity adhesives. During the dispensing process of the automatic dispensing machine, due to the high viscosity, it is particularly prone to produce wire-like protrusions, resulting in poor fluidity and severe wire-like protrusions, which affects the appearance. So how to solve this problem? Let's take a look together next.
If the company has very strict requirements for product quality, the hardware aspect can be considered. Pipes and valves are equipped with special valves for high-viscosity fluids, such as imported spiral valves. The viscosity value of the glue is provided to the manufacturer, and the manufacturer can help you provide the type of viscosity value to achieve the best dosing effect. Of course, for the spiral valves with high viscosity, the price is relatively expensive, but it can help you solve the drawing problem.
Among the various operations of the automatic dispensing machine, the following methods can be used to reduce or eliminate:
1. Enable glue delay
When the cap is opened, there is no glue between the glue outlet and the valve. If there is no glue between the distance, the rubber outlet opens and the movement will immediately start, which will cause a brief pause. The problem with the amount of glue formed may lead to wire drawing. To prevent this, after opening the glue, there will be a delay for a period of time, waiting for the glue to flow out, and then the subsequent distribution action will be carried out.
2. Glue Delay
After the cap is sealed, there is still no glue flowing between the cap opening and the glue valve. If the cap is moved immediately after it is sealed, there may be glue trailing and stringing. To prevent this from happening, after the cap is sealed, wait for a period of time for the glue to flow, and then perform the subsequent distribution operation.
3. Wire drawing height
Due to the high viscosity of certain adhesives (such as yellow glue and hot melt glue), the glue can be drawn out at a constant speed without damaging the glue track.
4. Lifting height
After the track is completed, move to the starting point of the next track. To prevent the rubber tip from hitting the pin, the glue is not aesthetically pleasing and it is even impossible to pull the pole. At the end point, raise the rubber tip to a certain height to ensure its safety and that it does not touch the pin. Then move to the starting point of the next section.
5. Close the glue ahead of time
In the continuous application of track glue, seal the rubber head before reaching the end. The remaining track is completed with residual pressure and remaining glue to prevent the end of the pile and stretching.
6. Ending the action
After the entire teaching trajectory is allocated, in order to facilitate the loading and unloading of the workpiece, improve processing efficiency or eliminate processing errors, the glue head can be moved to the designated position, or the starting point processing file can be handled, or the end point of the file processing can be handled, or reset, or the gear connection can also reduce the deep drawing problems caused by processing errors.
7. Lean upwards and lift up
Due to the adhesive property of the glue, the direct drawing action after the glue is closed cannot achieve the effect of breaking the glue line, or the shape of the glue line does not meet the requirements. Therefore, after the glue head is closed, a diagonal pulling preparation for stretching is carried out, which can prevent stretching.
8. Heating of Glue
The manufacturer of the dispensing machine reminds that it is advisable to heat the glue to an appropriate temperature to enhance its fluidity, thereby effectively addressing the wire drawing issue. Please be cautious not to set the heating temperature too high.
About
Introduction case Video Honor partner plantProduct
Automatic IC Programmer Automatic screw machine Automatic soldering machine Automatic dispensing machine More productsNews
Dynamic information FAQCustomer Service
ContactTel:+86 134-3400-6949
Copyright © 2026 Copyright © Guangdong Chengbo Intelligent Technology Co., Ltd.
The web page materials and related resources on this site are all sourced from the Internet. If there is any infringement, please notify us immediately. We will delete them within 24 hours.